- Home
-
AHU EC Fan Energy-saving Retrofit
- Belt-driven fan direct upgrade to ec direct drive
- Coupling-type fan upgrade to ec direct drive
- Independent temperature control & speed regulation retrofit solution
- Ba system linked intelligent retrofit
- Fixed frequency constant speed to variable frequency stepless speed regulation
- Special retrofit solution for clean workshops
- General retrofit solution for commercial buildings
- Industrial process air conditioning retrofit solution
- Non-stop lossless retrofit solution
- Standardized complete unit replacement solution
- Custom adaptive retrofit solution
-
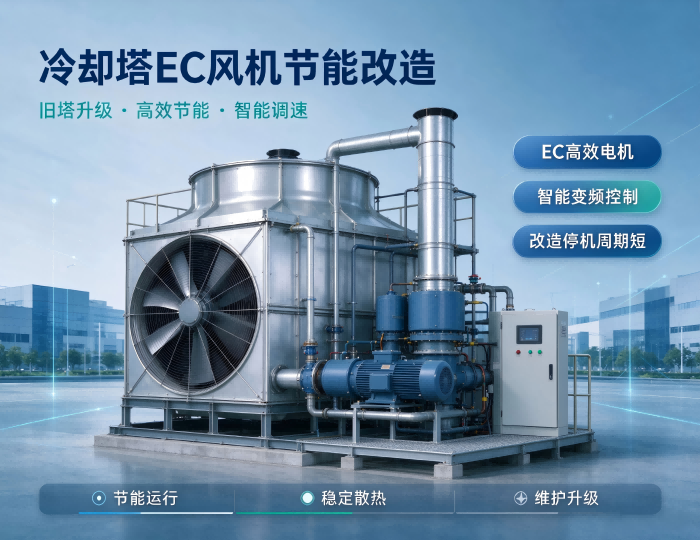
Cooling Tower EC Fan Energy-saving Retrofit
- Cooling tower ec fan conventional process retrofit
- Cooling tower ec fan non-stop lossless retrofit
- Cooling tower ec fan standardized complete unit replacement
- Cooling tower ec fan custom adaptive retrofit
- Cooling tower ec fan explosion-proof special retrofit
- Cooling tower multi-tower cluster linkage control retrofit
- Data Center Fan Wall
- EC Fan Box Energy-Saving Retrofit
- Cases
-
Product
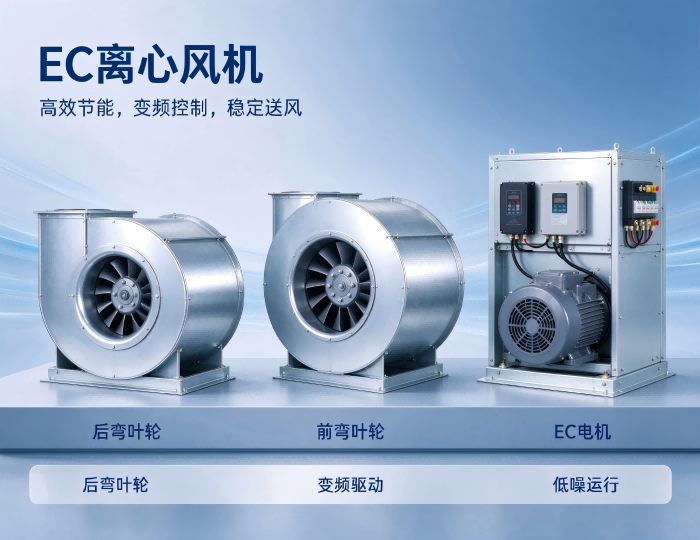
- EC Centrifugal Fan
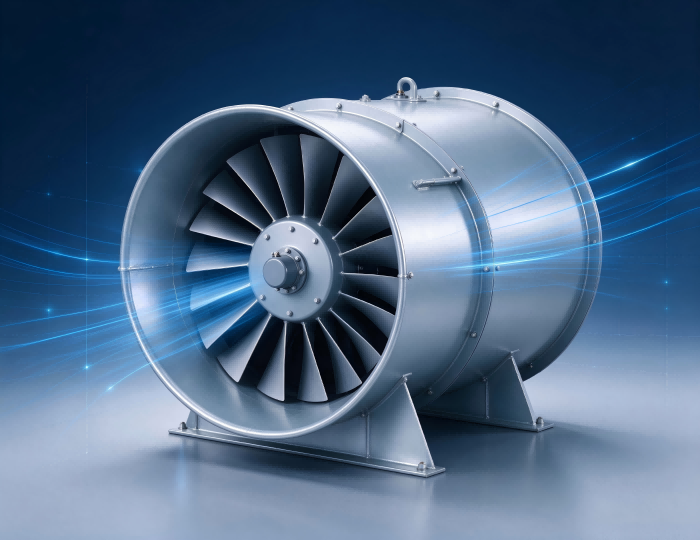
- EC Axial Fan
- EC mixed flow fan
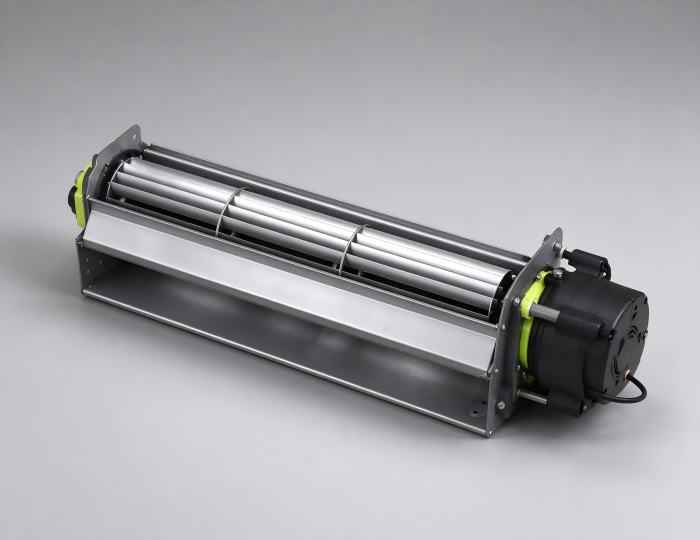
- EC cross flow / tangential fan
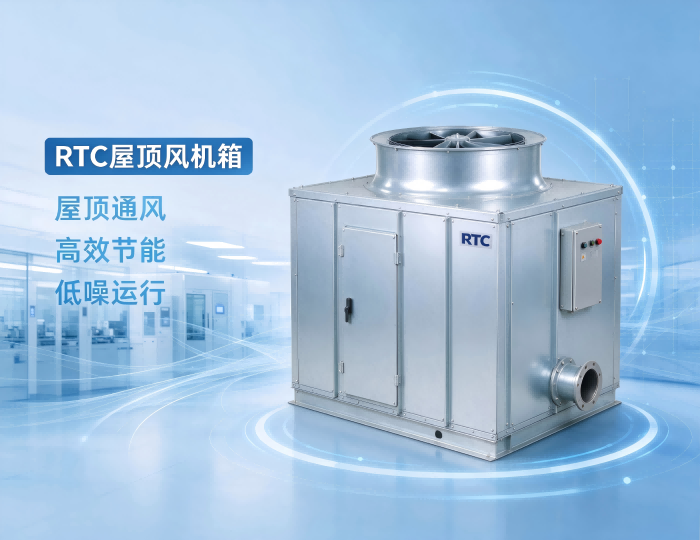
- RTC roof fan box
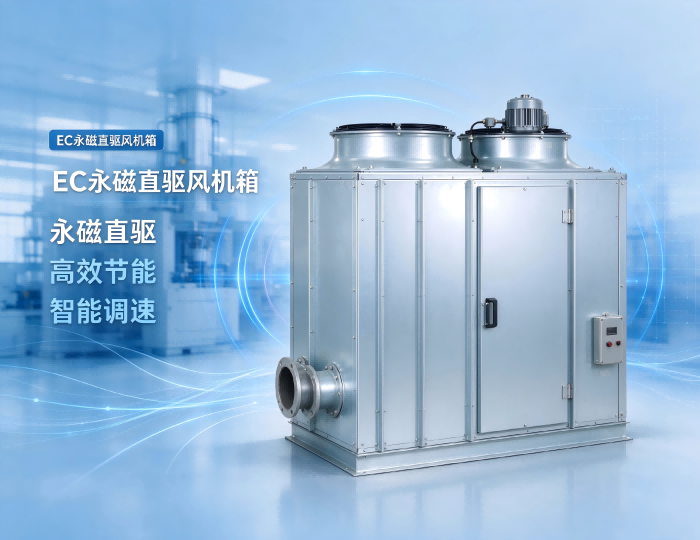
- EC permanent magnet direct drive fan box
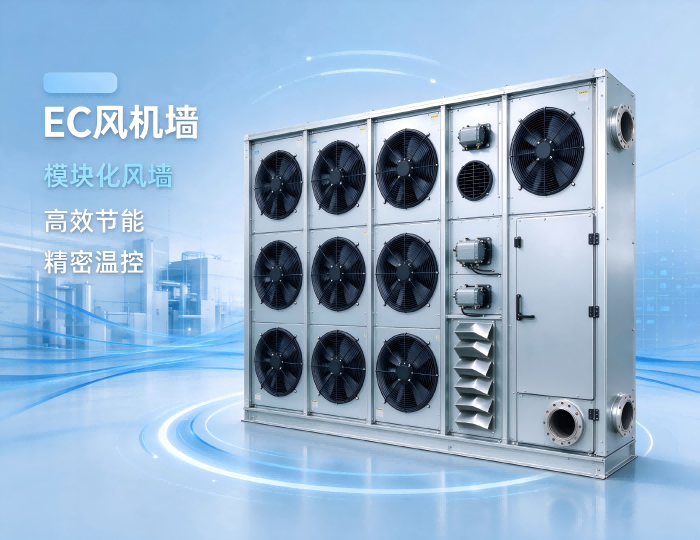
- Chilled water fan wall
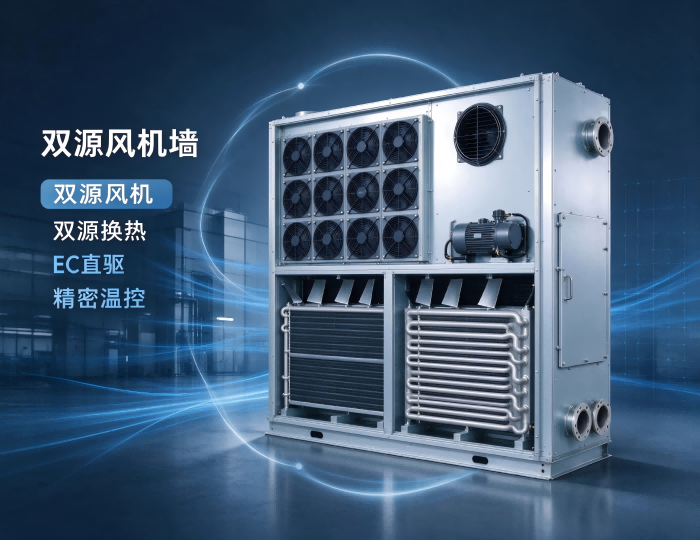
- Dual-source fan wall
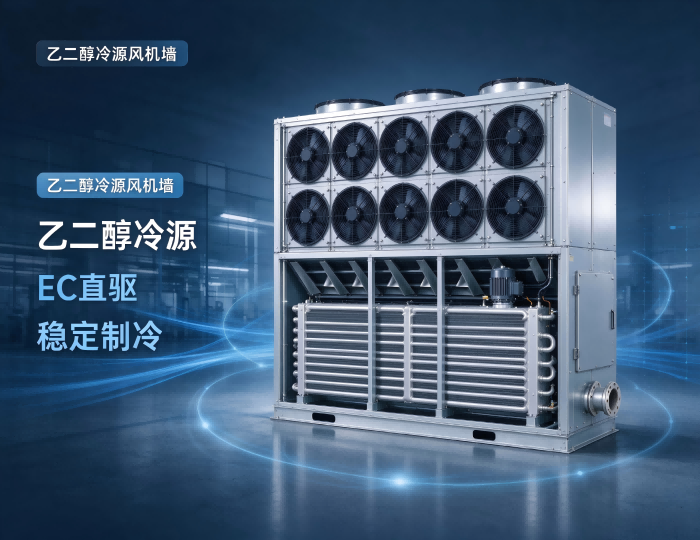
- Glycol cold source fan wal
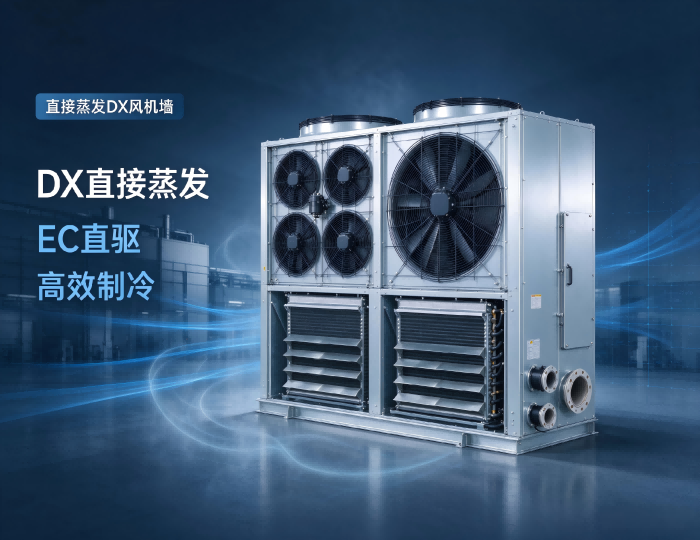
- Direct expansion (dx) fan wall
- Large Industrial Ceiling Fan
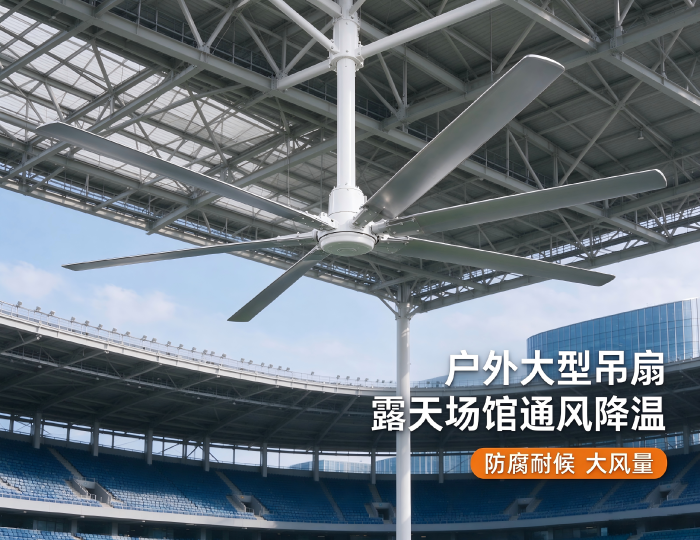
- Outdoor Large Ceiling Fan
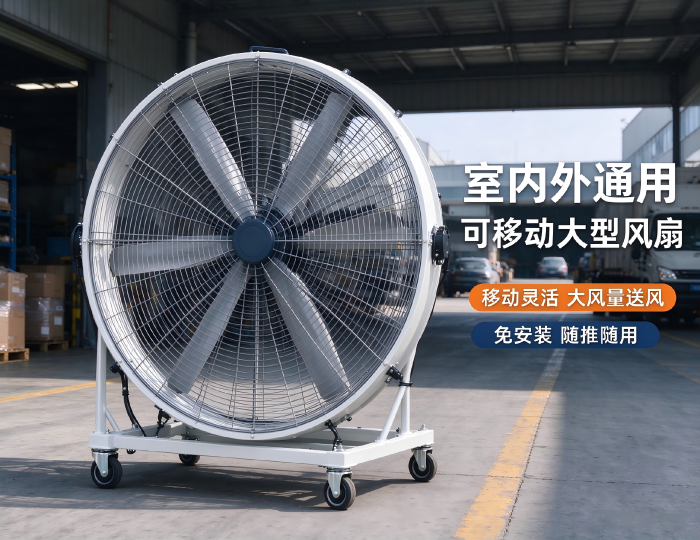
- Indoor‑Outdoor Universal Movable Large Fan
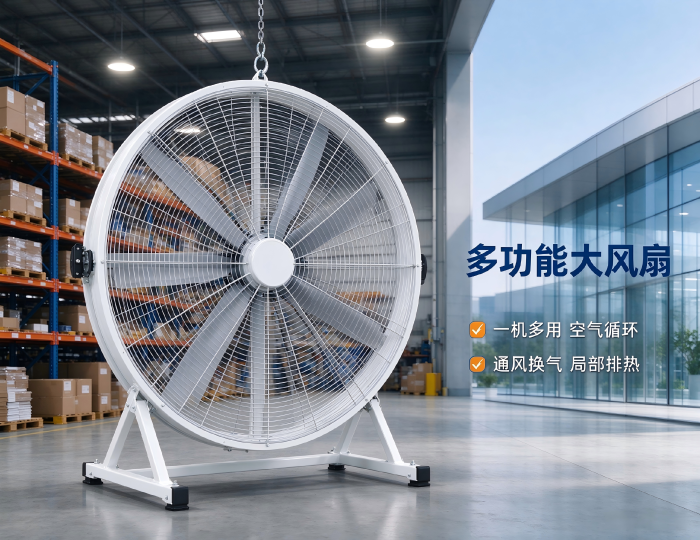
- Multi‑Functional Large Fan
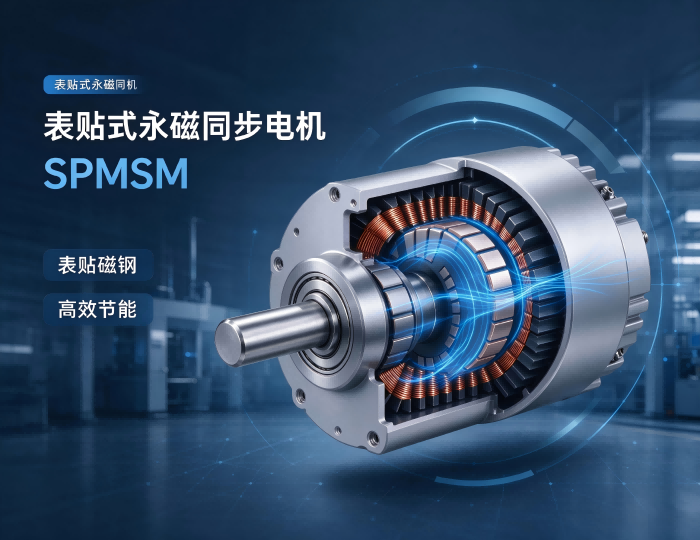
- Surface-mounted permanent magnet synchronous motor (SPMSM)
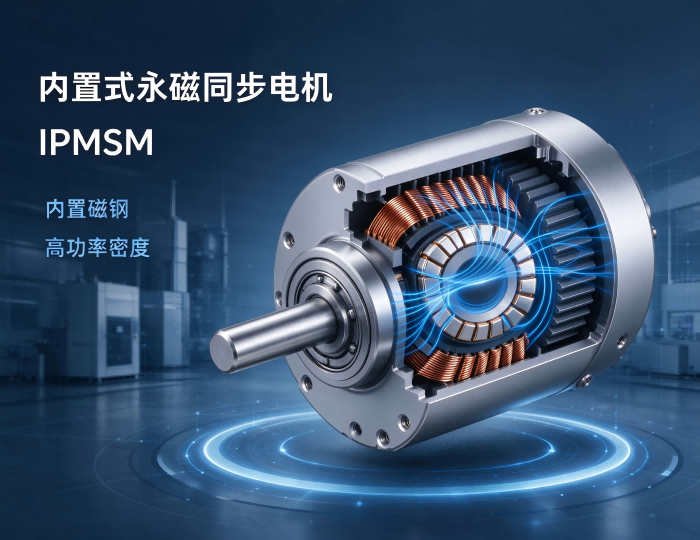
- Interior Permanent‑Magnet Synchronous Motor (IPMSM)
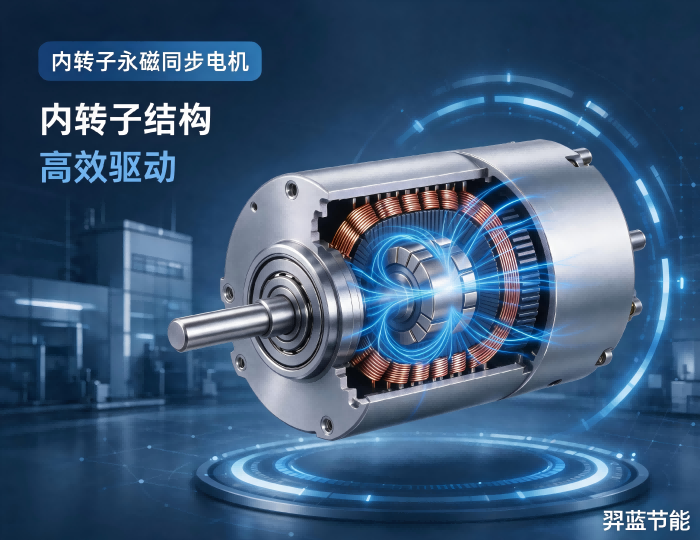
- Inner‑Rotor Permanent‑Magnet Synchronous Motor
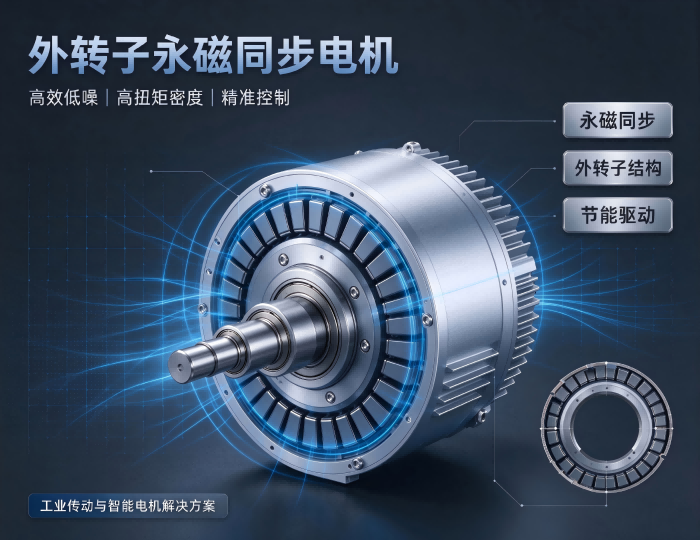
- Outer‑Rotor Permanent‑Magnet Synchronous Motor
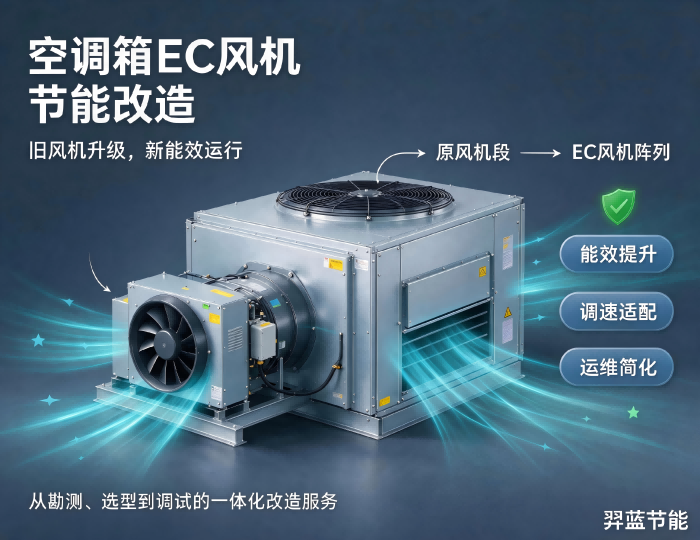
- Air‑Handling Unit EC Fan Energy‑Saving Retrofit
- Cooling Tower EC Fan Energy‑Saving Retrofit
- About Eblue






 1. High‑efficiency IE5‑grade EC motors: